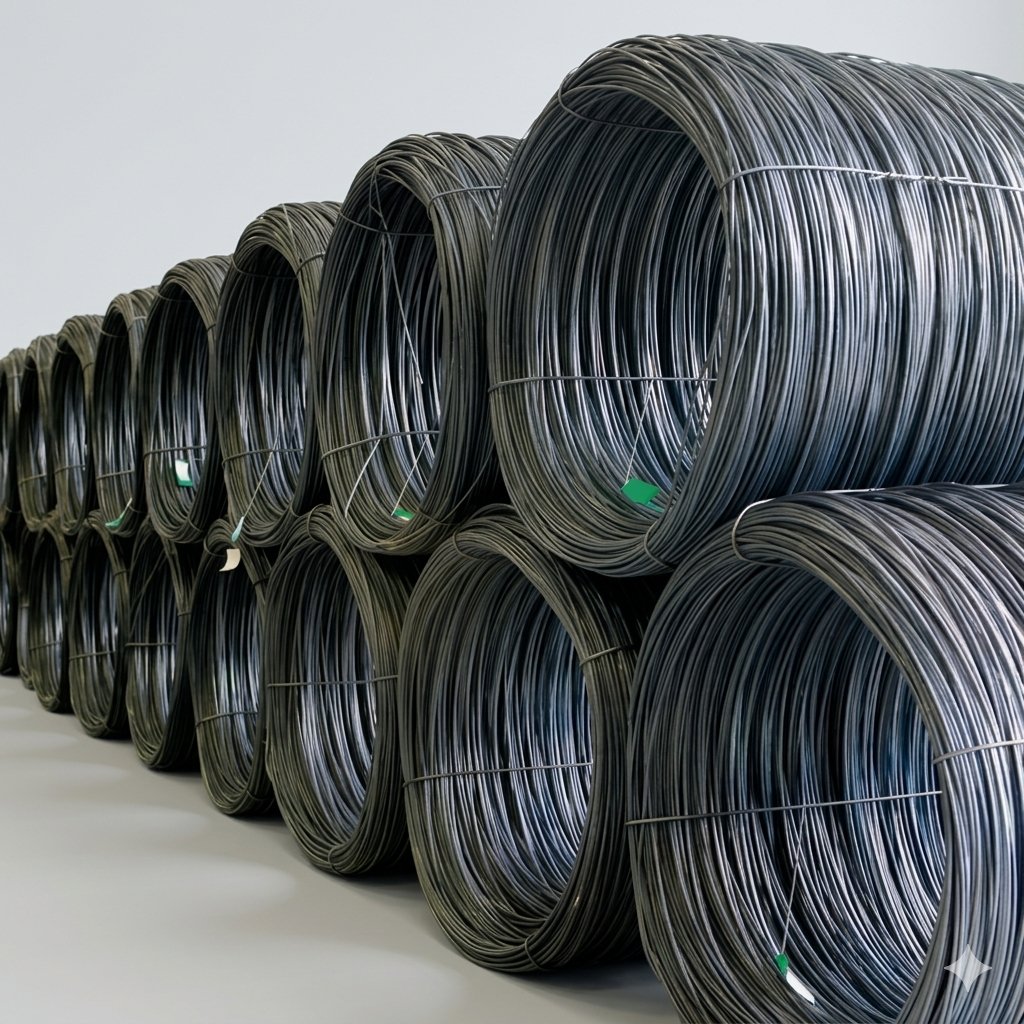

Industrial Hot-Rolled Wire Rod Coils & Carbon Steel Drawing Stocks
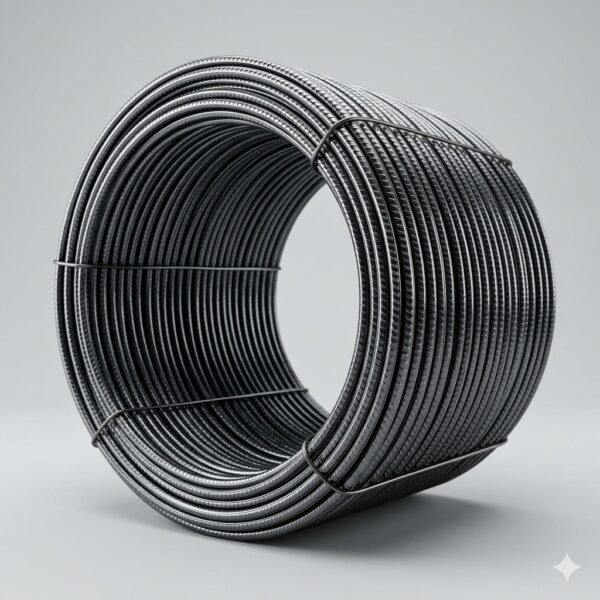
Our premium-grade wire rod coils selection represents the absolute metallurgical and physical benchmark for advanced continuous cold wire drawing, automatic mesh welding, structural concrete reinforcement fabrication, industrial fastener micro-heading, and high-tensile wire spring winding. Engineered precisely to comply with strict international B2B technical plant specifications and metallurgical manufacturing codes, these hot-rolled steel coils function as the primary raw material base for downstream multi-stage wire reduction complexes. By converting high-purity blast furnace melts into dimensionally uniform, macro-concentric steel coils, our wire rods ensure uniform mechanical characteristics and minimal tensile fluctuations, enabling your high-speed drawing blocks to run at maximum volumetric efficiencies with zero thread-snapping downtime.
As an authoritative global manufacturer and direct exporter of premier long steel products, our production facility coordinates automated continuous rolling trains, computerized Stelmor controlled cooling lines, and advanced hydraulic coil compression compactors. This specialized production sequence guarantees impeccable dimensional diameter constants, zero ovality distortions along the rod cross-sections, and loose scale characteristics that facilitate rapid, cost-efficient chemical or mechanical descaling loops. Whether your enterprise handles volume wholesale warehouse distribution across regional steel service hubs, or procures directly for tier-one wire mesh production frameworks, our hot-rolled wire rod lines provide uncompromised mechanical safety boundaries, certified trace metallurgical batch files, and highly competitive cost-to-volume ratio structures.
Core Engineering Strengths of Our Wire Rod Coils
1. Stelmor Controlled Cooling for Superior Cold-Drawing Ductility
In continuous high-speed multi-block wire drawing, microscopic structural inconsistencies can cause catastrophic thread-snapping failures. Our wire rods are conditioned via precision air-cooled conveyor systems after the final rolling block. This yields an optimized ferrite-pearlite matrix that maximizes structural elongation and reduction of area, allowing the metal to pass through progressive tungsten carbide drawing dies with minimal mechanical resistance.
2. High Precision Dimensional Diameter & Ovality Tolerance Controls
Irregular rod diameters and cross-sectional ovality can introduce severe friction loads during initial scaling passes, shortening die life. We employ advanced online infrared gauge tracking arrays that scan rod profiles at millisecond intervals, keeping diameter tolerances strictly within ±0.15mm and ovality within 0.20mm to guarantee flawless mechanical scaling transitions.
3. Optimized Scale Composition for Rapid Chemical and Mechanical Descaling
Before wire drawing can occur, the hot-rolled mill scale must be cleanly stripped. By regulating our air-cooling parameters, we manipulate the scale thickness and mineral layer balance. The resulting iron oxide layer splits away rapidly during mechanical reverse-bending descaling setups or dissolves completely within minimal chemical acid pickling cycles, dropping your factory chemical disposal expenditures.
4. Verified Pure Chemistry Compliant with ASTM & SAE Standards
We source raw metal melts strictly from top-tier blast furnaces to block unstable scrap iron mixtures that introduce fragile slag inclusion points. By preserving uniform, pure carbon-manganese element density distributions, our low-carbon (SAE1006/1008) and high-carbon (SAE1065/1080) wire coils provide predictable tensile boundaries, sound structural homogeneity, and exceptional heat-treat responses.
Technical Specifications & Wire Rod Ordering Matrices
We provide full customizable capabilities to support your target bidding frameworks and regional market demands. Review our standardized architectural specifications below:
| Technical Properties | Low Carbon Cold-Drawing Series | High Carbon / Welding Electrode Series |
|---|---|---|
| Available Steel Grades | SAE 1006, SAE 1008, Q195, Q235, SWRM8 | SAE 1065, SAE 1080, ER70S-6, SWRH62B/72B |
| Standard Diameter Span | 5.5 mm, 6.5 mm, 8.0 mm, 10.0 mm | 5.5 mm – 16.0 mm (Custom Calibrations Available) |
| Diameter & Ovality Tolerances | ±0.15 mm | Ovality ≤ 0.20 mm | ±0.20 mm | Ovality ≤ 0.25 mm (ASTM A510 compliant) |
| Individual Coil Weights | 1.8 Tons – 2.2 Tons per packed roll | 2.0 Tons – 2.5 Tons (Heavy Industrial Compacted) |
| Coil Geometric Profile | ID: 850mm | OD: 1250mm | Length: 1500mm | ID: 900mm | OD: 1250mm | Length: 1600mm Base |
| Mechanical Elongation | ≥ 30% (Excellent cold ductility matrix) | Optimized Per Grade Criteria (High reduction profiles) |
| Surface Scale Finish | Loose Oxide Scale (Sa 1 standard mill finish) | Controlled Wustite Scale Film (Phosphating ready) |
| Compliance Frameworks | ASTM A510, EN 10017, ISO 16120-2, GB/T 14981 | Full Mill Certification (MTC 3.1) & SGS Compliance |
Primary Global Drawing & Hardware Applications
Our structural hot-rolled wire rod coils operate as primary material feeding stocks specified by metallurgical processing plants and parts fabricators across massive global sectors:
- Continuous High-Speed Cold Drawing Mills: Fed natively into horizontal multi-die drawing blocks to manufacture bright annealed carbon wires, galvanized tying wires, construction tie filaments, and fine micro-meshes.
- Welded Wire Mesh & Rebar Fabrications: Straightened and cold-rolled into ribbed profiles inside automated grid welding machinery to construct heavy concrete reinforcement meshes, highway security fences, and logistical storage pallets.
- Fastener Stamping & Progressive Cold Heading: Sourced in specialized spheroidized-annealing-ready qualities to shear and continuously stamp common steel nails, dry-wall screws, structural bolts, heavy rivets, and wood fasteners.
- Fastener Stamping & Progressive Cold Heading: Sourced in specialized spheroidized-annealing-ready qualities to shear and continuously stamp common steel nails, dry-wall screws, structural bolts, heavy rivets, and wood fasteners.
B2B Bulk Supply Chain Quality Control & Ocean Freight Logistics
We tailor our shipping packaging protocols to securely transport high-tonnage concentrated steel payloads while insulating active rod loop faces from marine moisture rust degradation and high-impact transit movement:
-
- High-Tension Quad-Strap Mechanical Coil Compacting: Wire rod bundles carry immense concentrated weights. We heavily compress each coil unit via industrial hydraulic compactors, securing loops using a minimum of 4 heavy-gauge steel structural strapping strands to stop uncoiling misalignments.
- Full Enclosure Anti-Moisture Marine Shrouding (Optional): For premium grades or long maritime voyages exposed to extreme salt-spray vapors, coils are fully shrouded inside thick water-repellent woven polymer outer covers with interior desiccant bags to block surface oxidation, ensuring a clean mill finish.
- High-Security Container Shoring & Steel Wire Choking: Our specialized shipping crew blocks and ties down steel coil bundles inside 20ft dry containers using reinforced timber chocks, heavy turnbuckles, and industrial steel wire rope systems, fully eliminating shifting slippage and avoiding port customs delay penalties.
Frequently Asked Questions (FAQ)
Q1: How does your Stelmor controlled cooling line technology explicitly prevent wire snapping during continuous multi-block drawing?
A1: Wire snapping occurs when uneven micro-structures or hard martensite phases form during post-rolling cooling. Our computerized Stelmor conveyor line uses high-volume air blowing fans to carefully regulate the cooling rate of the moving rings. This uniform temperature drop ensures a high percentage of fine pearlite and soft ferrite throughout the steel matrix. This metallurgic consistency maximizes the area reduction limit, enabling your blocks to draw 5.5mm rods down to sub-millimeter filaments safely without requiring intermediate heat treatments.
Q2: What are the distinct application and drawing capability differences between SAE 1006 and SAE 1008 steel grades?
A2: The primary difference lies in the micro-carbon concentration constraints. SAE 1006 features a maximum carbon threshold of 0.08%, providing an exceptionally soft, ductile matrix with high elongation properties, making it the industry standard for micro-fine wire drawing (e.g., producing ultra-thin mesh filaments or galvanized binding wires under 1.0mm). SAE 1008 carries a slightly higher carbon limit of 0.10%, which increases yield strength and structural hardness. It is optimal for standard mesh wires, concrete reinforcement grids, construction nails, and stamped fasteners where higher shear resistance is required.
Q3: How does your factory modify the mill scale composition to optimize mechanical reverse-bending descaling operations?
A3: Traditional mill scale can be highly adherent, fracturing drawing dies if mechanical descaling fails. By injecting high-velocity cooling air right after the finishing block, we maximize the formation of a porous Wustite (FeO) layer while suppressing tight Magnetite (Fe3O4) skins. When your raw coils feed into a modern mechanical reverse-bending descaling roll array, this brittle Wustite layer fractures and releases cleanly from the metal core, leaving a clean surface ready for powdered lubricants without requiring intensive acid pickling tanks.
Q4: What is your typical factory minimum order quantity (MOQ) and production turnaround for full container bulk allocations?
A4: For standard global commercial diameters in common draw grades (such as standard 5.5mm or 6.5mm coils in SAE 1008 configurations), our baseline production factory MOQ is a full 20ft container allocation (roughly 20 to 25 metric tons to optimize maritime freight metrics), with logistics loading finishing inside 10 to 14 days post deposit confirmation. For custom high-carbon wire grades like SAE 1085, unique diameter adjustments, or specialized welding wire formulations, lead times average 20 days to balance furnace batch configurations and machinery adjustments.
Get Factory-Direct Wholesale Price & Free Samples
Are you searching for a stable, high-capacity Chinese manufacturer to optimize your procurement costs? Partner with us for premium Wire Rod Coils featuring heavy-duty, uniform mechanical performance, and superior drawability. We ensure full compliance with international fastener manufacturing, high-tensile wire drawing, rebar mesh fabrication, and automotive spring steel standards, backed by seamless global supply chain service.
- Flexible Tiered Pricing: Enjoy massive discounts and competitive FOB/CIF/CFR quotes for full container loads (20GP/40HQ) or bulk vessel shipments to maximize your inventory or manufacturing budget.
- 100% Free Samples: Test our steel quality firsthand. We offer premium Wire Rod Coil section samples (available in low/medium/high carbon steel, alloy steel, and stainless steel) featuring precise dimensional tolerances, uniform scale distribution, low inclusion levels, and excellent cold-heading properties. Perfect for wire drawing mills, fastener factories, or industrial metal wholesale verification.
- Guaranteed Fast Lead Time: Our advanced high-speed continuous wire rod rolling mills, Stelmor controlled cooling systems, automatic compacting and tying lines, and online eddy current testing equipment ensure prompt manufacturing and on-time shipment.
- Customized Packaging: Prevent coil unravelling, deep nesting deformation, or heavy sea-water corrosion during long-distance ocean transit. We use heavy-duty high-tensile steel wire straps (4+4 banding), weather-proof protective wrapping, anti-rust coatings, and sea-freight optimized loading on sturdy dunnage for safe port handling.